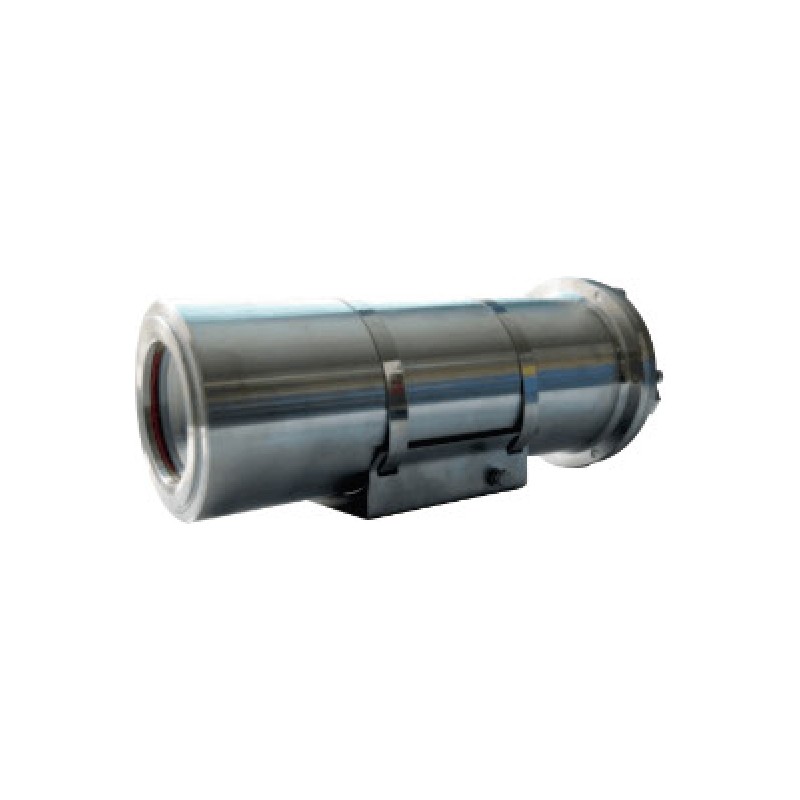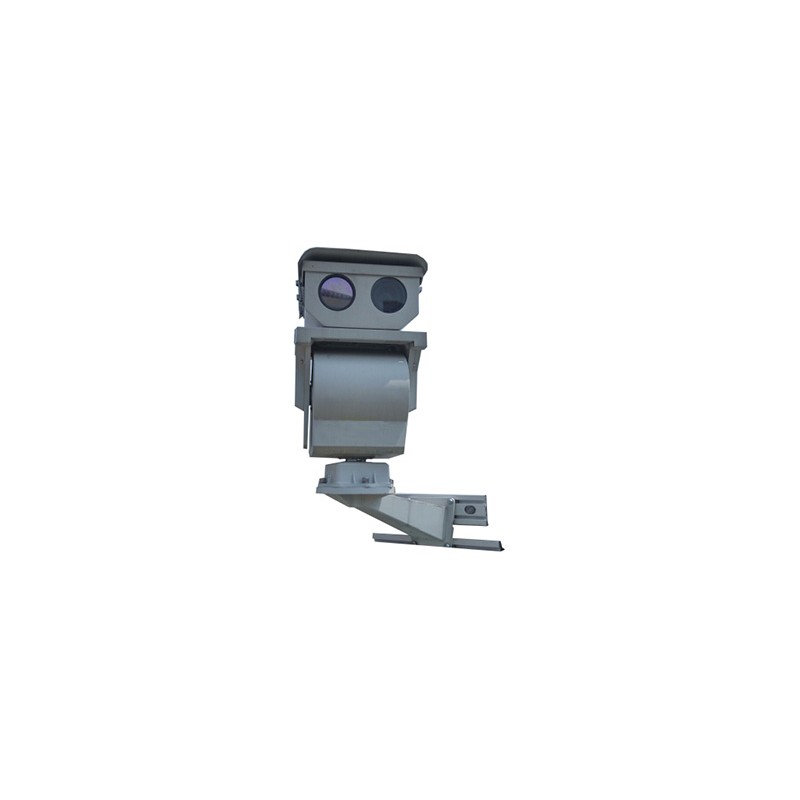


As one of the leading thermal imaging camera manufacturers, Changzhou Luming specializes in developing and producing high-performance infrared imaging cameras and comprehensive explosion proof camera solutions for extreme industrial environments. Our industrial thermal imaging cameras integrate advanced infrared detection technology, delivering accurate temperature measurement (±1°C), real-time thermal profiling, and predictive maintenance capabilities for applications in petrochemical, power generation, and metallurgical industries. The explosion-proof video cameras feature ATEX/IECEx-certified housings, corrosion-resistant stainless steel construction, and seamless integration with industrial control systems (Modbus, OPC UA), ensuring reliable 24/7 monitoring in hazardous areas (Zone 0/1).
Why Choose Our Thermal & Explosion-Proof Solutions?
Customizable thermal imaging camera system: OEM/ODM customization with end-to-end technical support.
Competitive Factory-Direct Pricing: Transparent explosion proof cctv camera price structures without compromising on safety standards.
Global Certifications: ATEX, IECEx, UL certified for Zone 0/1/2 hazardous locations.
Complete Hardware Ecosystem: Fully compatible with industrial-grade explosion proof monitor and control units.
Critical Applications for Hazardous Areas
Our security camera with thermal imaging capabilities are widely deployed in high-risk facilities to prevent disasters before they occur:
Petrochemical Tank Farms: Continuous thermal profiling of storage tanks to detect abnormal heat buildup.
Perimeter Protection: Functioning as an advanced infrared security camera system to detect intrusions in zero-light or heavy fog conditions.
Substation & Power Grid: Real-time hotspot detection on transformers and switchgears.
Enhance operational safety and efficiency with our integrated video-infrared-thermal camera system.